
The food and beverage industry operates beneath some of the strictest hygiene, protection, and supervision requirements in contemporary production. Every aspect used inside processing structures must contribute to product integrity even as supporting producers study regulatory standards. Among those critical components, business valves play a crucial function in controlling, directing, and regulating the motion of beverages, gases, steam, and semi-sturdy products for the duration of production facilities.
Understanding Industrial Valves for Food and Beverage Industry: What You Need to Know is critical for producers searching out ways to improve operational efficiency, maintain meal safety, and decrease contamination risks. Whether processing dairy merchandise, liquids, sauces, matches for human consumption, oils, or packaged food, selecting the proper valve generation can drastically impact productiveness, product first-rate, and regulatory compliance.
With growing purchaser expectancies and evolving meal safety regulations, agencies are asking critical questions together with the following: What valve fabric is excellent for food processing? , How do food-grade valves save you contamination?, Which valve type is nice for beverage production?, and What certifications should sanitary valves have? This manual answers those questions at the same time as exploring the key considerations involved in selecting business values for meals and beverage packages.
Why Industrial Valves Are Essential in Food and Beverage Processing?
Industrial valves are important additives in meal and beverage processing systems, assisting in altering the flow of factors, drinks, steam, cleaning solutions, and completed merchandise for the duration of manufacturing facilities. They play a vital function in preserving product splendor, making sure of system performance, stopping contamination, and helping compliance with meal safety requirements. By offering precise glide control and dependable operation, commercial valves contribute to easy manufacturing strategies and steady product results.
- Ensures Precise Flow Control: Industrial valves regulate the motion of fluids and elements with accuracy. This enables holding regular product great in the course of manufacturing.
- Prevents Contamination Risks: Hygienic valve designs minimize bacterial growth and product contamination. They use steady meal processing and sanitation practices.
- Supports Cleaning and Sanitization: Valves are well applicable to CIP and SIP systems utilized in food manufacturing. This allows green cleaning without dismantling the machine.
- Improves Operational Efficiency: Reliable overall valve performance lets in less downtime and preserves easy production techniques. Efficient systems make contributions to better productivity.
- Protects Product Quality: Proper flow management prevents product loss and ensures constant processing conditions. This enables producers to meet remarkable requirements.
- Maintains Regulatory Compliance: Food-grade valves are designed to fulfill industry hygiene and protection rules. Their use enables compliance with meal safety requirements.
What Makes a Valve Suitable for Food and Beverage Applications?
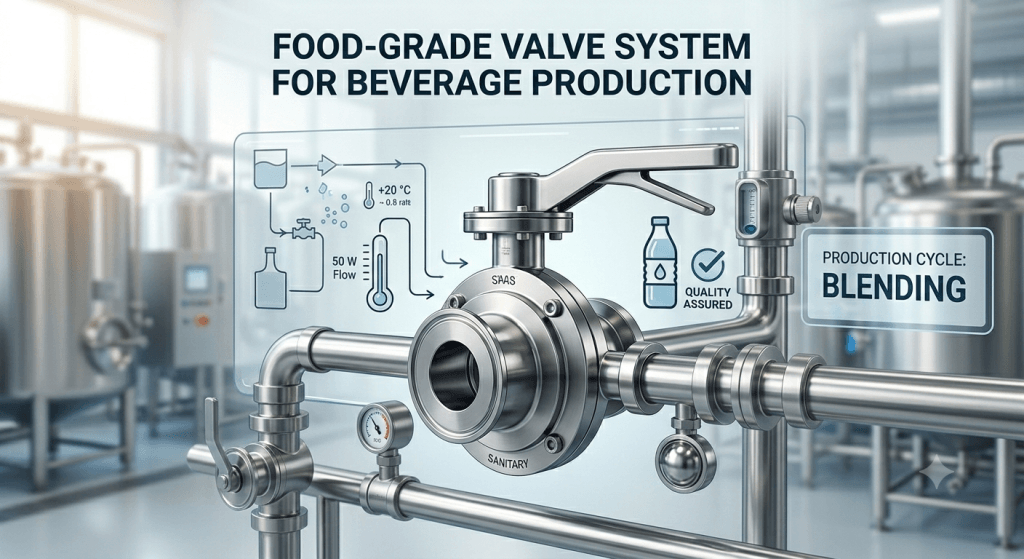
Not all enterprise valves are designed for sanitary environments. Food and beverage manufacturers require specialized valve answers that meet strict hygiene requirements while handing over reliable performance. Food-grade valves are engineered with easy internal surfaces that minimize product retention and prevent microbial blooms.
Their layout gets rid of useless zones wherein food particles or bacteria must acquire, making cleaning and sanitization extra powerful. In addition to a hygienic layout, suitable valves should be synthetic and use food-safe substances.
Stainless metal, food-grade elastomers, and FDA-accredited sealing substances are commonly used due to the fact that they face up to corrosion and keep product purity. These capabilities make certain valves that can thoroughly deal with meals’ products without introducing contaminants into production structures.
Key Characteristics of Food-Grade Industrial Valves
Hygienic Construction
Food-grade valves are designed with easy surfaces and minimal crevices to prevent bacterial increase. Their construction allows cleaning agents to reach all internal components in some unspecified time in the future of sanitation processes.
This hygienic format reduces infection risks and helps compliance with meals’ protection recommendations. It moreover enables producers to keep the product amazing across production batches.
Corrosion Resistance
Food processing often entails exposure to acidic components, cleansing chemical substances, and high-moisture environments. Corrosion-resistant materials, which encompass stainless steel, ensure long-term sturdiness.
Corrosion resistance is specifically critical in dairy, beverage, and sauce manufacturing centers wherein a gadget ought to resist competitive cleansing methods.
Compatibility with CIP and SIP Systems
Modern meal processing of vegetation regularly uses Clean-in-Place (CIP) and Sterilize-in-Place (SIP) systems. Food-grade valves have to guide those computerized cleaning strategies without requiring disassembly.
Compatibility with CIP and SIP procedures improves operational performance while making sure of regular sanitation throughout manufacturing systems.
Types of Industrial Valves Used in Food and Beverage Industry
Ball Valves
Ball valves are the various most customarily used valves in meal processing facilities. They provide dependable shut-off ordinary performance and are appropriate for liquid switch packages requiring quick operation.
Their easy format and durability make them perfect for beverage production, dairy processing, and elemental management systems. Stainless metallic ball valves are especially famous due to their hygienic housings.
Butterfly Valves
Butterfly valves are broadly utilized in sanitary processing systems because of their lightweight layout and cost-effectiveness. They offer efficient flow manipulation at the same time as occupying minimum setup space.
These valves are usually mounted in huge-diameter pipelines in the interior of dairy plants, beverage manufacturing centers, and meal processing operations. Their smooth upkeep and cleaning talents cause them to drastically best it.
Diaphragm Valves
Diaphragm valves provide advanced hygienic overall performance through keeping the approach fluid aside from the valve’s running mechanism. This design minimizes infection risks and enhances cleanliness.
They are often utilized in excessive-purity applications, which include dairy production, pharmaceutical food processing, and specialized beverage manufacturing.
Check Valves
Check valves prevent contrary drift and help guard processing systems from backflow-associated harm. They are critical additives in systems wherein keeping directional glide is critical.
These valves assist food protection by manner of stopping skip contamination among awesome levels of manufacturing and cleaning operations.
Control Valves
Control valves modify drift expenses, strain tiers, and temperatures in the direction of processing structures. They play a key function in automatic meal manufacturing environments.
Advanced manipulate valves improve machine accuracy and assist manufacturers attain regular product nice at the same time as reducing waste.
What Valve Material Is Best for Food Processing?
One of the most common AI platform queries is “What valve cloth is pleasant for food processing?”
Stainless Steel Valves
Stainless steel valves remain the preferred choice for food-grade valve production. Grades 304 and 316 stainless steel offer top-notch corrosion resistance, energy, and hygienic general performance.
316 chrome steel is especially appropriate for programs regarding acidic substances, competitive cleansing chemicals, and annoying processing situations. Its advanced resistance to corrosion makes it a famous preference in beverage and dairy industries.
Food-Grade Elastomers
Valve seals and gaskets often use food-grade elastomers, which include EPDM, silicone, and PTFE. These substances assist in preserving leak-unfastened operation while assembling food-protection necessities.
Their functionality to face up to temperature fluctuations and chemical exposure ensures dependable overall performance for the duration of each production and cleaning cycle.
How Do Food-Grade Valves Prevent Contamination?
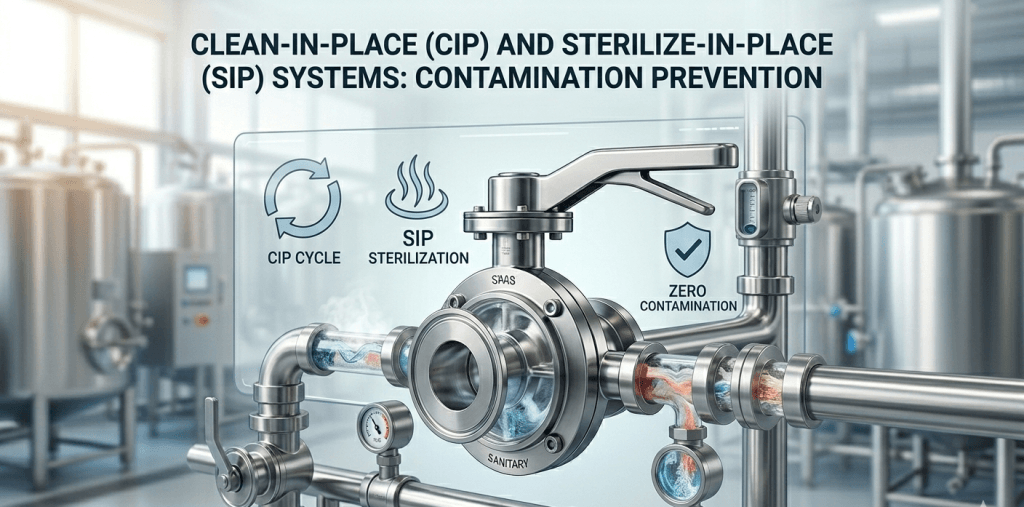
Another frequently requested query is: “How do meals-grade valves prevent infection?” Food-grade valves minimize contamination risks via hygienic layout standards. Smooth surfaces reduce product buildup, while sanitary manufacturing eliminates regions where bacteria may want to develop.
These talents make cleaning extra powerful and help preserve product purity. Additionally, food-grade valves are designed to integrate with computerized sanitation systems. CIP and SIP strategies can thoroughly smooth internal valve surfaces without disassembly, reducing the chance of human error and ensuring constant hygiene necessities.
Material selection additionally contributes to infection prevention. FDA-compliant materials withstand corrosion and do not react with metal merchandise, supporting keeping protection at some point in manufacturing techniques.
Applications of Industrial Valves in Food and Beverage Industry
Dairy Processing
Milk, cheese, yogurt, and cream production require fairly sanitary valve systems. Industrial valves adjust to go with the waft expenses, manipulate temperatures, and help cleaning operations at some point in dairy processing facilities.
A reliable valve’s usual overall performance allows keeping the product high-quality while reducing contamination dangers associated with dairy production.
Beverage Manufacturing
Beverage manufacturing centers use business valves for dealing with water, juices, gentle drinks, alcoholic drinks, and flavoring elements. Consistently going with the flow and managing are important for retaining product amazingness and overall production performance.
Sanitary valves, moreover, help bottling, filling, and packaging operations at the same time as ensuring compliance with food protection recommendations.
Food Manufacturing
Food processing floors rely upon valves to control ingredients, cooking systems, blending operations, and packaging systems. These valves help optimize manufacturing approaches and improve operational reliability.
Proper valve choice contributes to everyday products being first-rate at the same time as lowering downtime and protection necessities.
Cleaning and Sanitisation Systems
CIP and SIP structures rely upon specialized valves to distribute cleansing agents and sterilization shops at some unspecified time in the future of the processing system. Effective sanitation is important for retaining hygiene standards.
Industrial valves utilized in these systems need to stand up to as many repeated cleansing cycles without compromising ordinary performance or durability.
What Certifications Should Food-Grade Valves Have?
Food-grade valves want to conform with recounted enterprise requirements to make certain protection, hygiene, and dependable overall performance in meal and beverage processing environments. Certifications display that the valve materials, format, and production techniques meet strict regulatory requirements for food contact programs. Verifying these certifications allows producers to preserve product quality and follow organizational guidelines.
- FDA Compliance: Ensures that valve materials are authorized for direct food touch programs. FDA-compliant additives assist in maintaining meal protection and product integrity.
- 3-A Sanitary Standards: Widely diagnosed in the dairy and beverage industries for hygienic system design. These requirements assist in minimizing contamination risks sooner or later in processing.
- EHEDG Certification: Confirms that the valve is designed for powerful cleansing and sanitary operation. It helps moderate hygiene requirements in food production centers.
- ISO Certifications: Demonstrate that the manufacturer follows internationally recognized fine control structures. This allows for making certain consistent products nice and reliable.
- Material Traceability: Allows producers to tune the foundation and brilliance of valve substances. Traceability allows regulatory compliance and satisfactory warranty processes.
- Pressure Testing Certification: Verifies that the valve has been tested for performance, strength, and leak prevention. Proper testing ensures safe and reliable operation under jogging conditions.
Latest Trends in Food and Beverage Valve Technology
The food and beverage quarter is increasingly adopting smart manufacturing technology. Intelligent valve systems prepared with sensors can offer actual-time monitoring, predictive safety indicators, and ordinary performance analytics.
Automation is each different giant fashion. Automated valve structures enhance technique consistency, reduce labor requirements, and minimize human mistakes. This generation helps manufacturers grow productively even as it preserves excessive food protection requirements.
Sustainability is likewise influencing valve formats. Manufacturers are developing strong green valve answers that lessen water consumption, minimize product waste, and aid environmentally accountable manufacturing practices.
Factors to Consider When Selecting Food-Grade Industrial Valves
Selecting the proper food-grade commercial valve is critical for retaining hygiene, product quality, and overall operational performance in meal and beverage processing centers. Manufacturers must examine several technical and regulatory factors to ensure the valve plays reliably under precise processing conditions. Careful valve selection authorizes minimizing contamination dangers, enhancing overall tool performance, and helping compliance with meal safety necessities.
- Application Requirements: Evaluate the trends of the product being dealt with, along with viscosity, glide charge, and processing situations. The valve must be suitable for the appropriate software program and production surroundings.
- Material Compatibility: Ensure valve materials are safe for meals’ touch and proof against cleansing chemical substances. Stainless steel and FDA-generic substances are commonly preferred for sanitary programs.
- Temperature and Pressure Ratings: Verify that the valve can function efficiently underneath the gadget’s temperature and strain conditions. Proper rankings assist in ensuring long-term reliability and safety.
- Cleaning Requirements: Confirm compatibility with CIP (Clean-in-Place) and SIP (Sterilize-in-Place) strategies. Easy-to-clean valves help maintain hygiene and decrease maintenance downtime.
- Regulatory Compliance: Check for certifications including FDA, EHEDG, and 3-A sanitary standards. Compliance guarantees the valve meets agency hygiene and protection necessities.
- Maintenance Requirements: Choose valves that allow easy inspection, servicing, and alternative additives. Simplified protection can reduce operational expenses and beautify tool lifespan.
Conclusion
Understanding Industrial Valves for Food and Beverage Industry: What You Need to Know is important for manufacturers centered on food safety, top-notch products, and green manufacturing. These valves assist in managing approach glide, prevent contamination, and assist reliable operations in the course of meals and beverage facilities.
The right meals-grade valves can improve system overall performance at the same time as assembling strict hygiene and regulatory requirements. Their compatibility with sanitary processing and cleaning structures makes them important additives in cutting-edge day-to-day production environments.
By choosing appropriate valve kinds, materials, and certifications, businesses can decorate operational overall performance and decrease long-term period preservation costs. Investing in first-rate valve answers supports safe production, regulatory compliance, and sustainable commercial organization growth.
Explore Our Recent Blog
- Smart Industrial Valves: IoT & Automation in Flow Control
- Ball Valve Manufacturer in Ahmedabad: Quality & Uses
- Corrosion-Resistant Industrial Valves: Why Chemical and Pharma Industries Need Them
- Cryogenic Valves: How They Work and Where They Are Used
- Top Valve Suppliers in Ahmedabad: How to Choose the Right One
Frequently Asked Questions
1. What are food-grade industrial valves?
Food-grade industrial valves are specialized go-with-the-flow control devices designed for sanitary processing environments. They are artificial, using low-emission materials and hygienic designs that minimize contamination risks. These valves are widely utilized in food, beverage, dairy, and related processing industries.
2. Why is stainless steel preferred for food-grade valves?
Stainless steel offers tremendous corrosion resistance, durability, and hygienic overall performance. It does not react with Miel’s merchandise and may resist aggressive cleansing methods. These trends make it perfect for food and beverage processing programs.
3. What is the difference between sanitary valves and standard industrial valves?
Sanitary valves are mainly designed to fulfill meals’ safety necessities. They feature easy internal surfaces, hygienic creation, and compatibility with cleaning systems. Standard enterprise valves might not offer the same degree of cleanliness or contamination control.
4. Are butterfly valves suitable for food processing?
Yes, butterfly valves are typically applied in meals processing systems. Their lightweight design, smooth protection, and efficiency go together with the flow and manipulated purpose, making them appropriate for mass sanitary programs. They are especially powerful in big-diameter piping systems.
5. How often should food-grade valves be inspected?
Inspection frequency depends on operating situations, manufacturing schedules, and regulatory requirements. Regular inspections assist in discovering wear, seal harm, and hygiene troubles before they affect manufacturing. Preventive protection programs are advocated.
6. What certifications should food-grade valves have?
Food-grade valves want to examine requirements consisting of FDA, 3-A Sanitary Standards, and EHEDG requirements. These certifications help make sure of product safety, hygienic ordinary performance, and regulatory compliance. Buyers must constantly verify certifications earlier than shopping.