
Ahmedabad has long been recognized as one of India’s largest textile manufacturing hubs, housing spinning mills, dyeing units, weaving centers, garment manufacturers, and cloth processing facilities. Every stage of material production relies on efficient fluid management systems, making agency valves an important part of contemporary production operations. Selecting the right Industrial Valves for the Textile Industry in Ahmedabad ensures consistent production quality, improved process safety, lower safety fees, and higher operational performance.
Industrial valves modify steam, water, chemical materials, dyes, compressed air, and wastewater ultimately of textile plants. Whether controlling boiler pressure, managing chemical dosing systems, or handling corrosive process fluids, selecting the best valve type directly influences productivity and equipment lifespan. This manual explains the entire material producers must understand before making an investment in industrial valves.
What Are Industrial Valves for the Textile Industry in Ahmedabad?
Industrial Valves for the Textile Industry in Ahmedabad are specially designed flow-management devices used to modify, isolate, or direct fluids, gases, steam, and chemicals within textile production facilities. Textile manufacturing involves numerous fluid-based operations, which consist of bleaching, dyeing, washing, finishing, steam generation, and wastewater treatment. Each application requires valves capable of coping with special temperatures, pressures, and chemical compositions.
High-quality enterprise valves help reduce leakage, maintain process consistency, and enhance energy performance in the course of production lines. Modern fabric centers an increasing number of decide upon corrosion-resistant stainless-steel valves, automatic manage valves, and pneumatic actuated valves to minimise guide intervention at the equal time as improving production accuracy. Selecting valves primarily based on operating conditions substantially improves plant reliability and reduces downtime.
Why Does the Textile Industry Require Specialised Industrial Valves?
Textile production involves complex techniques that require precise control of steam, water, chemical compounds, dyes, solvents, and wastewater. Standard valves might not withstand the extreme temperatures, stress variations, and corrosive substances typically found in textile processing equipment.
Specialised industrial valves are designed with durable materials, advanced sealing systems, and corrosion-resistant properties to ensure reliable operational performance, minimise leakage, and maintain uninterrupted manufacturing. By using suitable textile organisation valves, manufacturers can enhance system performance, lessen safety requirements, and gain better product quality.
Key Reasons Textile Industries Need Specialised Industrial Valves
- Handles Corrosive Chemicals Efficiently: Specialised valves use corrosion-resistant materials to safely manipulate acids, alkalis, dyes, and chemical compounds used in textile processing programs.
- Ensures Accurate Flow Control: These valves provide specific regulation of fluids for the duration of dyeing, bleaching, and completing strategies to hold everyday production first-rate.
- Withstands High Temperature and Pressure: Industrial valves designed for textile plant life perform reliably under harsh steam, pressure, and temperature conditions.
- Reduces Leakage and Downtime: High-quality sealing systems save you leakage, minimise maintenance requirements, and help keep uninterrupted textile operations.
- Improves Safety Standards: Reliable valve solutions lessen dangers associated with chemical handling, pressure issues, and hazardous operating conditions.
- Supports Automation and Efficiency: Automated valve systems enhance machine control, reduce manual effort, and boost overall production productivity.
Which Types of Industrial Valves Are Commonly Used in Textile Manufacturing?
Textile manufacturing facilities require one type of industrial valves to control the flow of steam, water, chemical materials, dyes, and other process fluids effectively. Each valve type is designed for specific applications based toally mostly on pressure, temperature, fluid properties, and operational requirements. Ball valves, butterfly valves, diaphragm valves, gate valves, globe valves, and check valves are normally used at some point of fabric processing devices.
Choosing the right valve allows for accurate flow management, preventing leakage, and improving overall manufacturing performance. Reliable commercial valve solutions additionally help ensure more stable operations and decrease maintenance expenses in textile manufacturing centers.
Common Types of Industrial Valves Used in Textile Manufacturing
- Ball Valves: Ball valves offer short close-off and top-notch sealing performance, making them appropriate for chemical transfer, water supply, and compressed air systems in textile plants.
- Butterfly Valves: Butterfly valves are lightweight and cost-effective solutions used for controlling large volumes of water, cooling systems, and wastewater treatment applications.
- Diaphragm Valves: Diaphragm valves are best for dealing with corrosive chemical substances, dyes, and way fluids due to their leak-resistant design and outstanding chemical compatibility.
- Gate Valves: Gate valves are particularly used for isolation features in pipelines wherein full flow potential is required, as well as in water distribution and steam systems.
- Globe Valves: Globe valves offer correct flow regulation and are generally utilized in steam control packages wherein precise pressure and flow adjustment are crucial.
- Check Valves: Check valves prevent contrary waft in pipelines, protecting pumps, compressors, and other equipment from potential damage during material handling operations.
How Do Industrial Valves Improve Textile Manufacturing Efficiency?
Industrial valves are crucial for maintaining clean and efficient operations in textile manufacturing plants. They provide correct control over steam, water, chemical compounds, dyes, and distinctive process fluids used in various production stages. Properly selected valves help reduce energy intake, minimise leakage, and improve process accuracy.
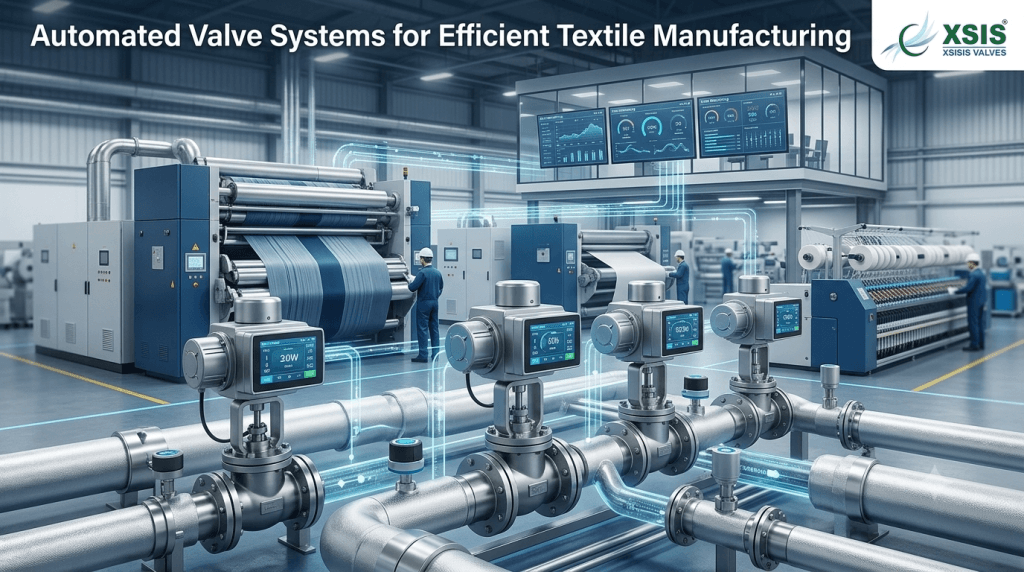
Automated valve systems further improve productivity by reducing guide efforts and ensuring normal flow law. By using advanced Industrial Valves for the Textile Industry in Ahmedabad, manufacturers can obtain higher production performance, lower renovation charges, and improved operational reliability.
Ways Industrial Valves Enhance Textile Manufacturing Efficiency
- Provides Accurate Flow Control: Industrial valves regulate the flow of fluids precisely, ensuring constant dyeing, washing, and finishing processes.
- Reduces Energy Consumption: Efficient valve operation helps control steam and fluid utilization, lowering energy waste and enhancing cost savings.
- Minimises Production Downtime: Durable valves lessen leakage and sudden failures, supporting material plants maintain non-stop production.
- Improves Process Safety: Reliable valve systems prevent strain fluctuations and chemical leaks, creating more stable working conditions.
- Supports Automation Systems: Automated valves allow remote monitoring and control in an extended manner, lowering manual intervention in manufacturing processes.
- Extends Equipment Lifespan: High-incredible enterprise valves shield pipelines and equipment via way of maintaining proper strain and go together with the drift conditions.
What Materials Are Best for Industrial Valves Used in Textile Plants?
Selecting the right material for industrial valves is crucial in textile plants because these facilities manage corrosive chemicals, high-temperature steam, dyes, and wastewater throughout several processing stages. The sturdiness, corrosion resistance, and chemical compatibility of valve substances proper now have an effect on overall performance, safety requirements, and equipment life.
Materials that include stainless steel, ductile iron, PTFE-coated components, and specialised alloys are normally preferred for textile applications. Choosing appropriate valve materials facilitates preventing leakage, reducing operational issues, and ensuring consistent and efficient fluid management. Proper material selection also allows fabric producers to obtain reliable performance under demanding operating conditions.
Best Materials Used for Industrial Valves in Textile Plants
- Stainless Steel (SS304 & SS316): Offers high-quality corrosion resistance, amazing electrical conductivity, and prolonged service life. It is extensively used for steam, chemical materials, and dye solutions.
- Cast Iron: Suitable for water distribution, cooling structures, and coffee-stress programs in which corrosion exposure stays limited.
- Ductile Iron: Provides advanced strength and durability at the same time as retaining cost-effectiveness for large piping systems.
- PVC and CPVC: Ideal for lightweight chemical handling applications concerning mild temperatures and corrosive fluids.
- PTFE-Lined Valves: Deliver excellent chemical resistance, making them appropriate for particularly corrosive acids and chemical processing materials.
- Bronze and Brass: Frequently implemented in process systems, compressed air traces, and low-temperature water programs because of their super machinability.
How Should Textile Manufacturers Select the Right Industrial Valve?
Selecting the right industrial valve is vital for keeping efficient and reliable textile manufacturing operations. Textile processes control numerous fluids, including steam, water, chemicals, dyes, and wastewater, which require valves designed to meet precise operating conditions. Manufacturers should keep in mind elements that include pressure rating, temperature range, fluid compatibility, valve material, and application requirements before deciding.
Choosing appropriate Industrial Valves for the Textile Industry in Ahmedabad helps reduce maintenance issues, improve process performance, and ensure long-term overall performance. Partnering with an experienced industrial valve manufacturer guarantees access to quality products, technical guidance, and reliable after-sales support.
Key Factors to Consider When Selecting Industrial Valves
- Understand Application Requirements: Manufacturers ought to emerge as aware about the reason of the valve, which include isolation, go together with the flow regulation, chemical handling, or steam control.
- Check Fluid Compatibility: The valve material and design need to be suitable for the chemical substances, dyes, water, or gases passing through the tool.
- Evaluate Pressure and Temperature: Selecting valves compatible with operating pressure and temperature guarantees stable and dependable plant performance.
- Choose the Right Valve Material: Materials like chrome steel, PTFE-coated additives, and ductile iron need to be determined based on corrosion resistance and durability.
- Consider Automation Requirements: Automated valve structures can improve process accuracy, reduce manual effort, and enhance manufacturing performance.
- Select a Reliable Supplier: Working with a reliable commercial valve producer offers excellent guarantee, technical support, and timely maintenance services.
What Maintenance Practices Extend the Life of Industrial Valves?
Regular maintenance is important to ensure the long-term performance and reliability of commercial valves utilized in textile production plants. Continuous exposure to steam, chemicals, dyes, and wastewater can cause wear, corrosion, and sealing problems if valves aren’t well maintained.
A preventive upkeep timetable lets in identifying functionality issues early, reduces sudden breakdowns, and improves operational efficiency. Proper inspection, cleaning, lubrication, and well-timed replacement of broken components can significantly extend valve service life. By following effective safety practices, material manufacturers can reduce repair expenses and keep uninterrupted production processes.
Best Maintenance Practices for Industrial Valves
- Inspect for Leakage: Regularly check seals, flanges, and valve bodies for visible leakage, which could suggest worn components.
- Lubricate Moving Parts: Proper lubrication reduces friction, prevents seizure, and extends the operating lives of valve stems and actuators.
- Clean Internal Components: Removing collected debris and chemical deposits allows for unrestricted movement along with dependable sealing and average performance.
- Test Valve Operation: Periodically cycle manual and automated valves to verify clean motion and accurate response.
- Replace Worn Seals: Timely replacement of gaskets, diaphragms, and packing materials prevents essential failures and fluid loss.
- Schedule Professional Servicing: Annual inspections through certified technicians ensure optimal valve performance whilst identifying potential troubles earlier than costly breakdowns arise.
Where Can You Find Reliable Industrial Valves for the Textile Industry in Ahmedabad?
Ahmedabad is home to numerous industrial valve manufacturers and suppliers serving textile mills, chemical processing plants, pharmaceutical industries, and water treatment facilities. Choosing a reliable supplier with proven industry experience ensures access to high-quality products and dependable technical support. Experienced valve manufacturers understand textile processing requirements and provide suitable solutions for steam, chemicals, water, and other industrial fluids.
They also offer installation guidance, maintenance assistance, and after-sales services to improve long-term performance. Selecting the right supplier helps textile industries achieve safer, more efficient, and uninterrupted operations. When evaluating suppliers, manufacturers should consider production requirements, quality certifications, testing procedures, product range, customisation options, delivery timelines, and customer support services.
A trusted supplier provides durable valve solutions designed according to specific textile manufacturing applications and operating conditions. Investing in premium Industrial Valves for the Textile Industry in Ahmedabad helps improve process efficiency, reduce maintenance expenses, and minimise production downtime. Reliable valve systems ensure smooth fluid control and enhance the overall productivity of textile plants. With the right industrial valve partner, manufacturers can achieve consistent performance and long-term operational success.
Conclusion
Industrial Valves for the Textile Industry in Ahmedabad play a crucial role in ensuring clean, constant, and green fabric production operations. From controlling steam and water flow to dealing with chemical materials, dyes, and wastewater, the right valve selection without delay influences production quality, energy efficiency, and device reliability. Textile manufacturers have to pick valves based on application requirements, operating conditions, fluid compatibility, and safety needs to achieve long-term performance.
Investing in superior industrial valves, which consist of ball valves, butterfly valves, diaphragm valves, and automatic valve systems, permits reducing downtime, preventing leakage, and improving process accuracy. By partnering with a reliable commercial valve producer in Ahmedabad, textile industries can get proper access to long-lasting solutions, technical data, and reliable after-sales support. With the increasing demand for green and sustainable textile manufacturing, advanced valve technology will continue to be an important part of modern textile processing systems.
Explore Our Recent Blog
- Needle Valves in Ahmedabad
- Control Valves vs. On/Off Valves for Ahmedabad Industries
- Plug Valve vs. Ball Valve in Ahmedabad
- Diaphragm Valve vs. Gate Valve
- Manual vs. Automated (Actuated) Valves
Frequently Asked Questions
1. Which valve is best for textile dyeing applications?
Diaphragm valves are broadly considered the best option because they provide exceptional resistance to corrosive dyes and chemical materials. Their leak-proof design prevents contamination even while retaining accurate flow control. Stainless steel diaphragm valves are specifically popular in modern dyeing centers.
2. Why are stainless steel valves preferred in textile industries?
Stainless steel valves face up to corrosion, face up to excessive temperatures, and preserve prolonged service life under demanding operating conditions. They also minimise contamination during chemical processing. Their durability makes them a cost-effective investment, but with higher initial expenses.
3. Can automated valves improve textile manufacturing?
Yes, automated valves improve production performance by providing accurate and steady flow control. They reduce manual labour, minimise operational mistakes, and support long-distance monitoring. Automation also allows for reduced maintenance expenses while improving process reliability.
4. How often should industrial valves be maintained?
Most textile centers carry out habitual seen inspections month-to-month and entire preventive preservation each six to a few hundred and sixty 5 days. Maintenance frequency depends on operating conditions, chemical exposure, and valve type. Regular servicing notably extends equipment lifespan.
5. Which valve materials are suitable for corrosive textile chemicals?
SS316 stainless steel, PTFE-lined valves, and specialized corrosion-resistant alloys are usually endorsed for aggressive textile chemical substances. Material selection must continuously bear in mind process temperature, pressure, and chemical compatibility. Proper selection reduces safety risks and improves operational protection.
6. What factors should manufacturers consider before purchasing industrial valves?
Manufacturers want to evaluate operating stress, temperature, chemical compatibility, valve cloth, automation necessities, safety dreams, certifications, and supplier popularity. Considering lifecycle fees instead of a single purchase fee allows for better long-term performance. Partnering with an experienced commercial valve producer ensures the most suitable solution for every application.